Most industrial conveyors are designed around a known load. Recycling and waste processing does not offer that. What lands on the belt is whatever came in on the truck, which on a given day means shredded metal, a length of rebar, wet material, a chunk of concrete, and something nobody can identify. The conveyor has to move all of it, continuously, without becoming the bottleneck.
That is a durability problem before it is a throughput problem, and it is the reason welded hinge steel belt is the right construction for these operations. A solid steel pan does not care what lands on it.
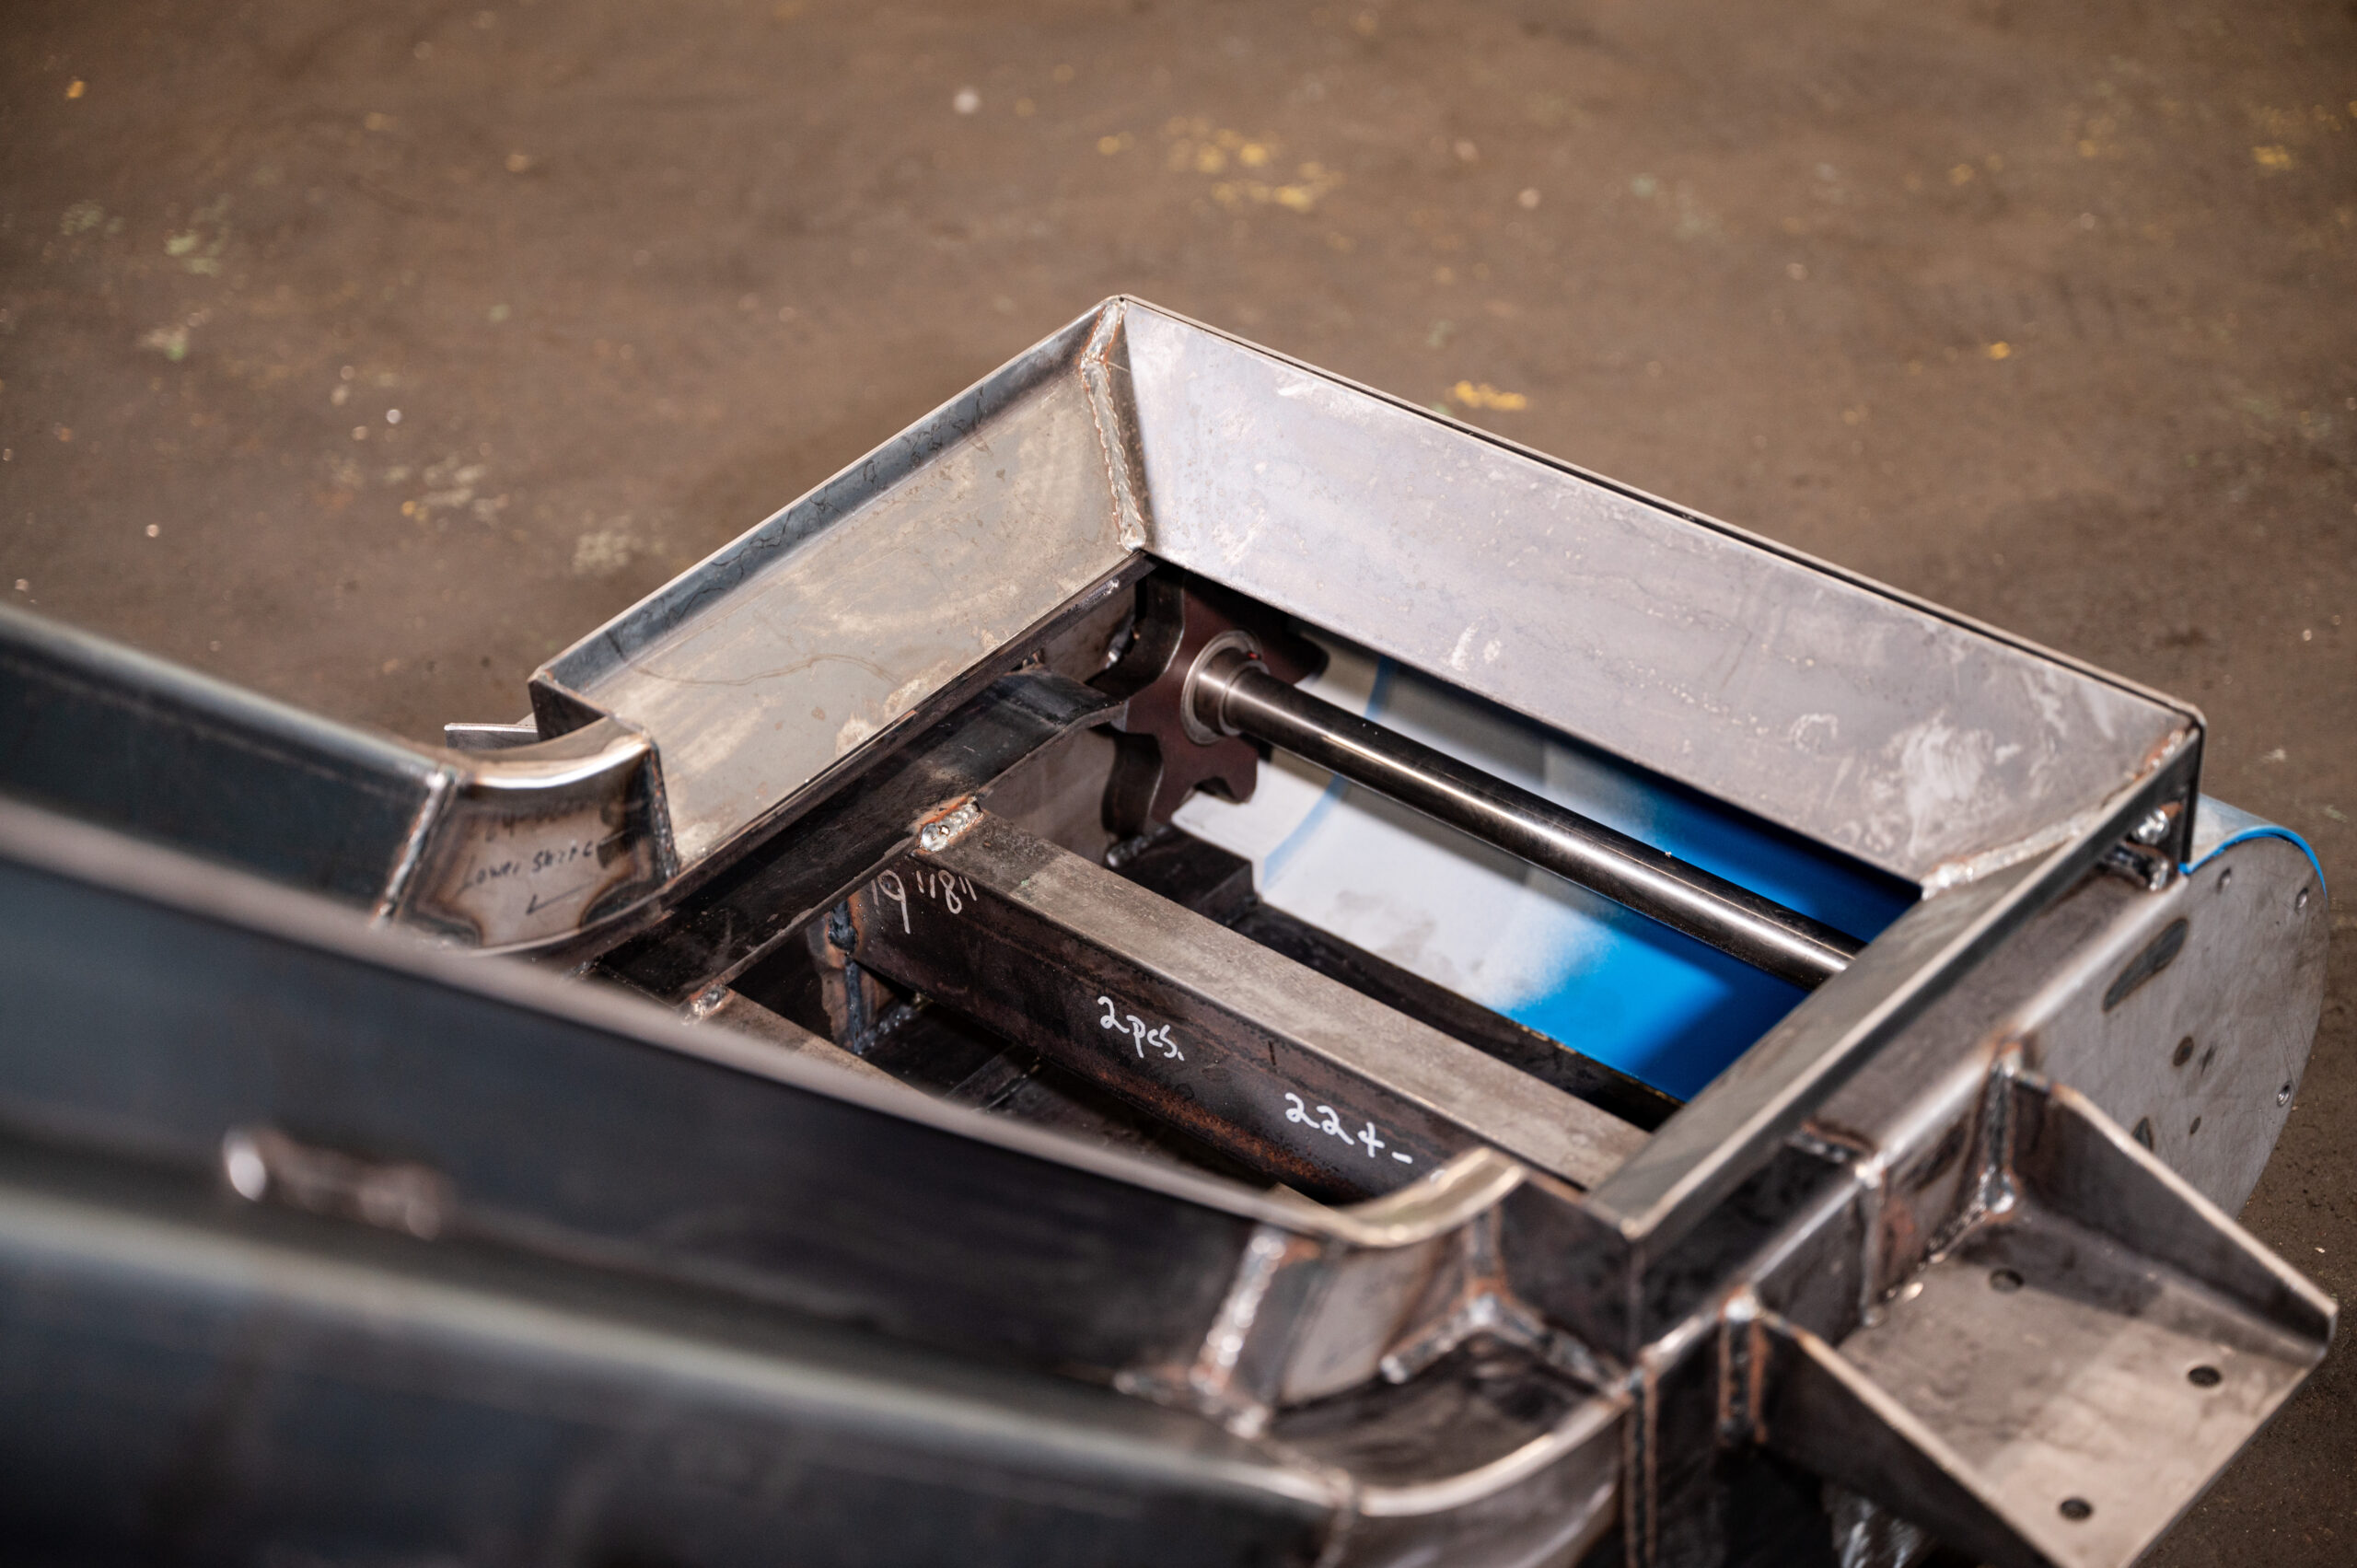
Impact, Abrasion, and Everything Else
Three things wear out a conveyor in a recycling operation, and they arrive together.
Impact. Material is loaded by grapple, loader bucket, or free fall from a shredder or hopper. The belt takes the full drop of whatever is being dumped, repeatedly, at whatever weight it happens to be. A belt that deforms under impact starts tracking badly, and a belt that tracks badly destroys everything it runs against.
Abrasion. Mixed loads carry grit, glass, concrete dust, and dirt. That mix does not simply ride on the belt, it grinds against the pans, the track, and the side skirting for the whole length of the run, every run.
Contamination. Moisture, dirt, and fines work into the chain, bearings, and drive components. That is a maintenance and lubrication issue as much as a design issue, and it drives choices about how accessible the wear points need to be.
Built for Continuous Duty
Recycling operations tend to run their equipment hard and long, so the specification leans heavier than it would for an equivalent throughput elsewhere. Pan thickness, track and liner selection, and side skirting all get set against abrasion rather than against the calculated load alone.
Belting and Frame
- 6″ and 9″ pitch typical for mixed and heavy loads
- Pans from 3/16″ up past 1″ thick where impact requires it
- Abrasion-resistant track liners
- Side skirting sized to the material and load method
- Loading baffles and hoppers at transfer points
Drive and Tensioning
- Shear pin hub on any pitch
- Optional drive monitoring through the conveyor controls
- Spring or air take-up for automatic tension on long continuous runs
- Screw take-up where ends are accessible for regular checks
- Cleats and wings sized to hold material on the incline
Jams Are the Expected Condition
In most industries a jam is a fault. In recycling it is a matter of when, because sooner or later something arrives that should not have. The design question is not how to prevent every jam but what happens when one occurs.
A shear pin hub or slip clutch stops the drive before the belt, sprockets, and reducer absorb the load, so an unexpected piece of rebar costs a pin rather than a gearbox. Where the line runs with limited supervision, monitoring built into the conveyor controls raises the fault immediately instead of leaving it to be discovered. Both approaches, and when each makes sense, are covered on our overload and jamming protection page.
Tension on Long Runs
Recycling conveyors are often long, inclined, and installed where neither end is easy to reach once the line is built around them. That makes take-up selection a real decision rather than a default. Screw take-ups are simple and inexpensive where somebody can get to the end and check tension on a schedule. Spring and air take-ups adjust automatically over the life of the belting and earn their cost where the conveyor is buried in the plant. The trade-offs are laid out on our take-up design page.
Rebuilds
A recycling conveyor frame frequently outlives several belts. We re-belt and rebuild conveyors regardless of the original manufacturer, so a worn unit in an established line is usually a replacement belt or a rebuild rather than a replacement, and the surrounding structure stays where it is.
Slat Belt Conveyors
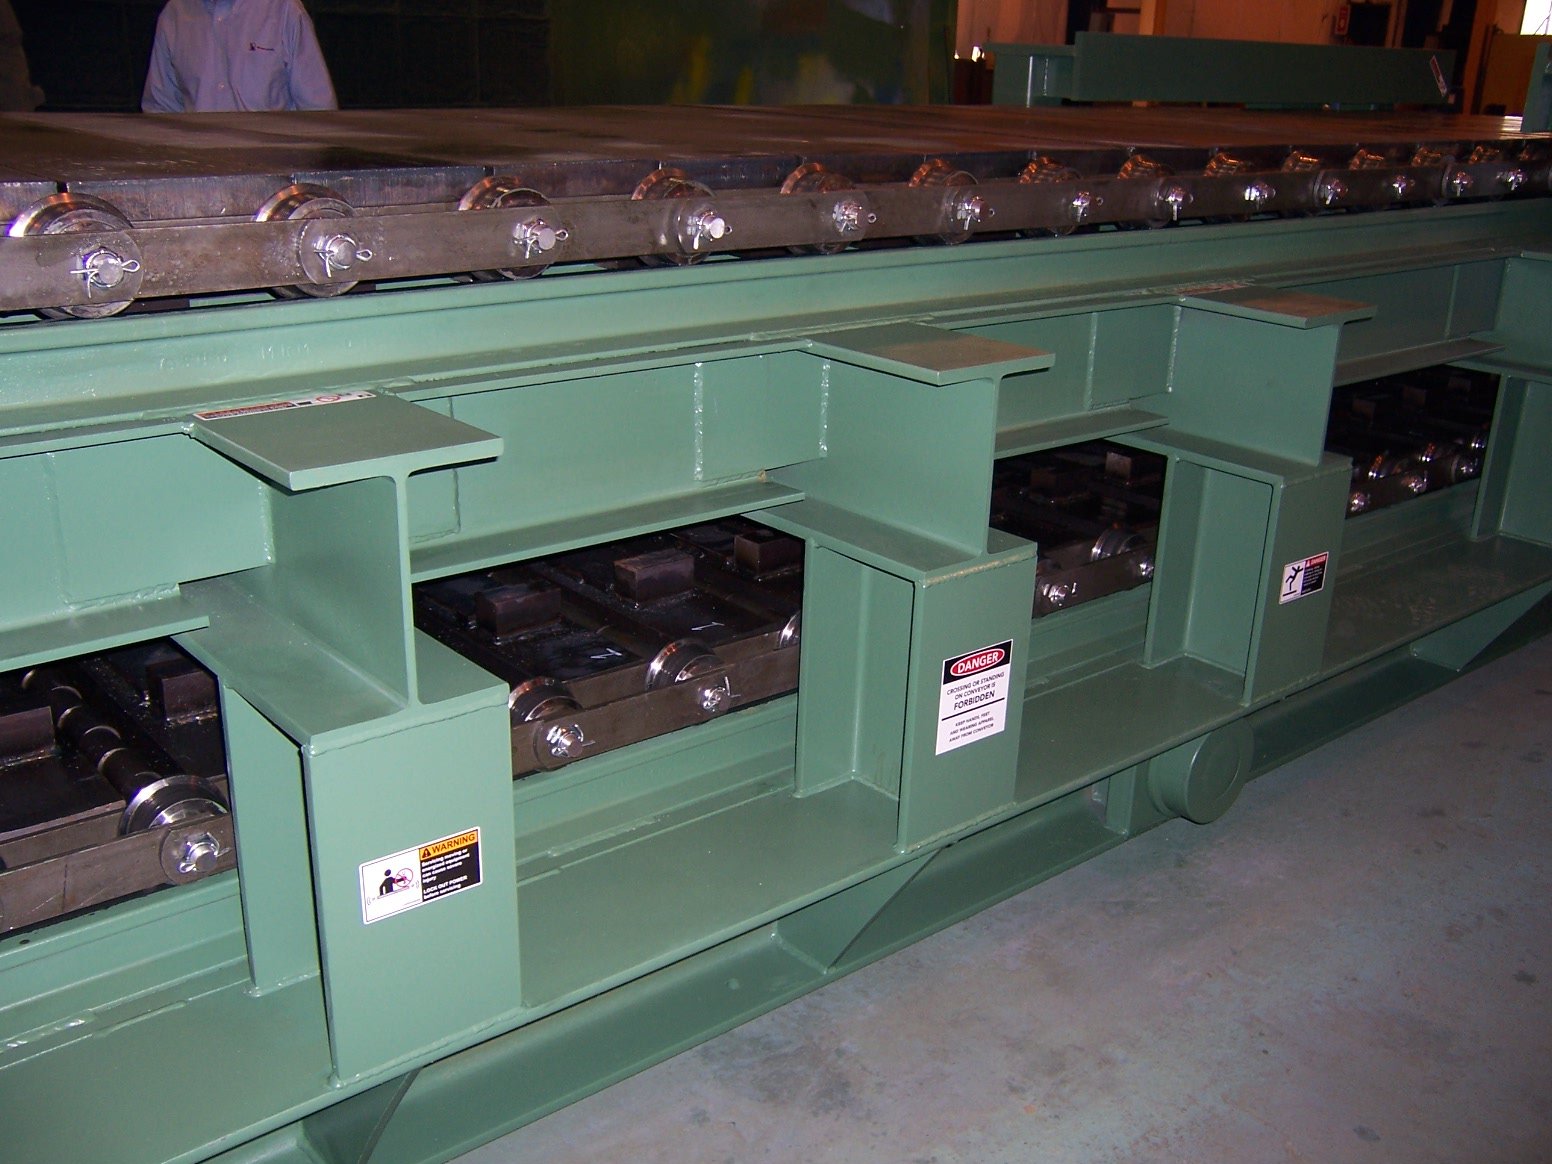
For the heaviest recycling loads, Transcon also builds slat belt conveyors: heavy steel slats mounted across heavy-duty chain. Slat width, slat thickness and chain pitch are all set by the material and how it is loaded. Slat belts are not something most conveyor builders supply.
Related Solutions
- Scrap Handling Systems - collection, elevation, and discharge
- Scrap Handling Technical Overview - configuration and specifications
- Slat Belt Conveyors - heavy steel slats for heavy, hot material
- Custom Conveyor Systems - for layouts nothing standard fits
- Conveyor Maintenance - keeping a hard-duty system running
Common Questions
Short answers to what engineers and maintenance teams ask us most about this equipment.
Can Transcon conveyors handle recycling and waste materials?
Yes. Our heavy-duty conveyor systems are well-suited for recycling and waste processing operations where equipment must handle varied, abrasive, and often unpredictable materials on a continuous basis. The durability of our welded hinge belt design - rated for up to 600 lbs/ft - makes it ideal for the demanding conditions in recycling facilities where conventional conveyors fail prematurely.
What overload protection is available on Transcon conveyors?
Mechanical protection comes first. A shear pin hub can be fitted to any size or style of Transcon conveyor, and a slip clutch is also available. Either one stops the drive before the belt, sprockets, and reducer absorb the load, so a jam costs a shear pin and a few minutes instead of a gearbox and a shift.
Monitoring through the conveyor controls can be added on top of that. Where a conveyor runs unattended, the controls can raise the fault to your line rather than leaving it to be discovered at shift change. Full detail on overload and jamming protection.
Can Transcon build conveyors for high-temperature applications?
Absolutely. Our welded hinge steel belt conveyors are specifically engineered for extreme heat environments like hot forging operations, where parts can reach several thousand degrees Fahrenheit. We use heat-resistant belt materials, reinforced frames for impact zones, high-temperature bearings, rollers, and drive components, plus specialized scale-handling chutes and collection sections. These systems integrate directly with furnaces, presses, and forge hammers.
Running a line that eats conveyors?
Tell us what you process, how it gets loaded, and how long the run needs to be. An engineer will tell you where the current system is failing and what it would take to stop replacing it.